Quality engineered into every batch.
Our quality systems, manufacturing infrastructure, & analytical capabilities are designed to meet the most stringent regulatory requirements, ensuring that every molecule we produce is reliable, repeatable, & ready to file.
Quality built in, not inspected in
We don't test quality into a batch at the end, we build it in from the first experiment. Quality control, analytical validation, & batch documentation run in parallel with synthesis, so every molecule arrives with the rigor regulators expect & customers deserve.
From synthesis to release, continuous assurance
Every batch undergoes rigorous quality control at multiple stages. In-process testing monitors reaction progression & validates critical parameters. Release testing confirms identity, purity, & strength. Comprehensive batch documentation creates an audit trail that regulators trust.
- ✓ In-process testing at reaction critical control points
- ✓ Release testing against approved specifications
- ✓ Full batch record documentation aligned with ICH guidelines
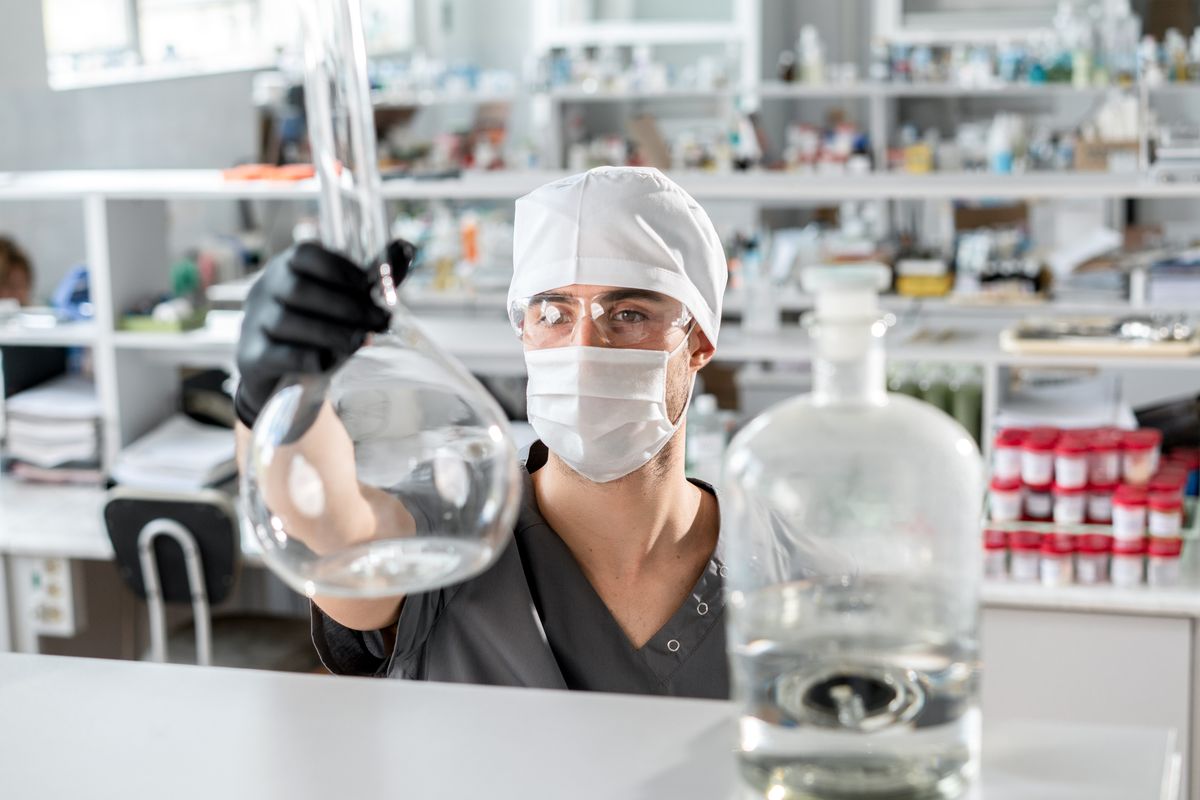 Quality control, integrated
Instrumentation for advanced characterization
Our analytical labs are equipped with state-of-the-art instruments for method development, validation, & impurity profiling, enabling rapid method deployment & regulatory-ready data packages.
HPLC Systems
High-Performance Liquid Chromatography for routine & method-development separations, impurity profiling, & purity assays.
GC & GC-FID
Gas Chromatography for volatile compound analysis, residual solvent testing, & trace-level impurity detection.
LC-MS / MS
Liquid Chromatography-Mass Spectrometry for structure confirmation, metabolite profiling, & advanced impurity identification.
NMR Spectroscopy
1H & 13C Nuclear Magnetic Resonance for structural elucidation & purity determination of organic compounds.
Polarimetry
Specific optical rotation measurement to confirm the chiral identity & purity of amino acids & their derivatives.
Karl Fischer & Melting Point
Moisture content by Karl Fischer titration & melting point determination for routine identity & release testing.
Designed for precision & scale
Our Hyderabad facility houses multiple multi-purpose reactors ranging from 10L to 500L capacity, supporting seamless scale-up from kilo-lab through pilot to commercial production. Separate areas for hazardous & non-hazardous chemistry, combined with dedicated support for amino acid synthesis, allow us to handle the full spectrum of ART Biochem's capabilities without cross-contamination.
- ✓ Multi-purpose reactors, 10L–500L capacity
- ✓ Kilo-lab to pilot-scale production capability
- ✓ Dedicated areas for hazardous chemistry & amino acid synthesis
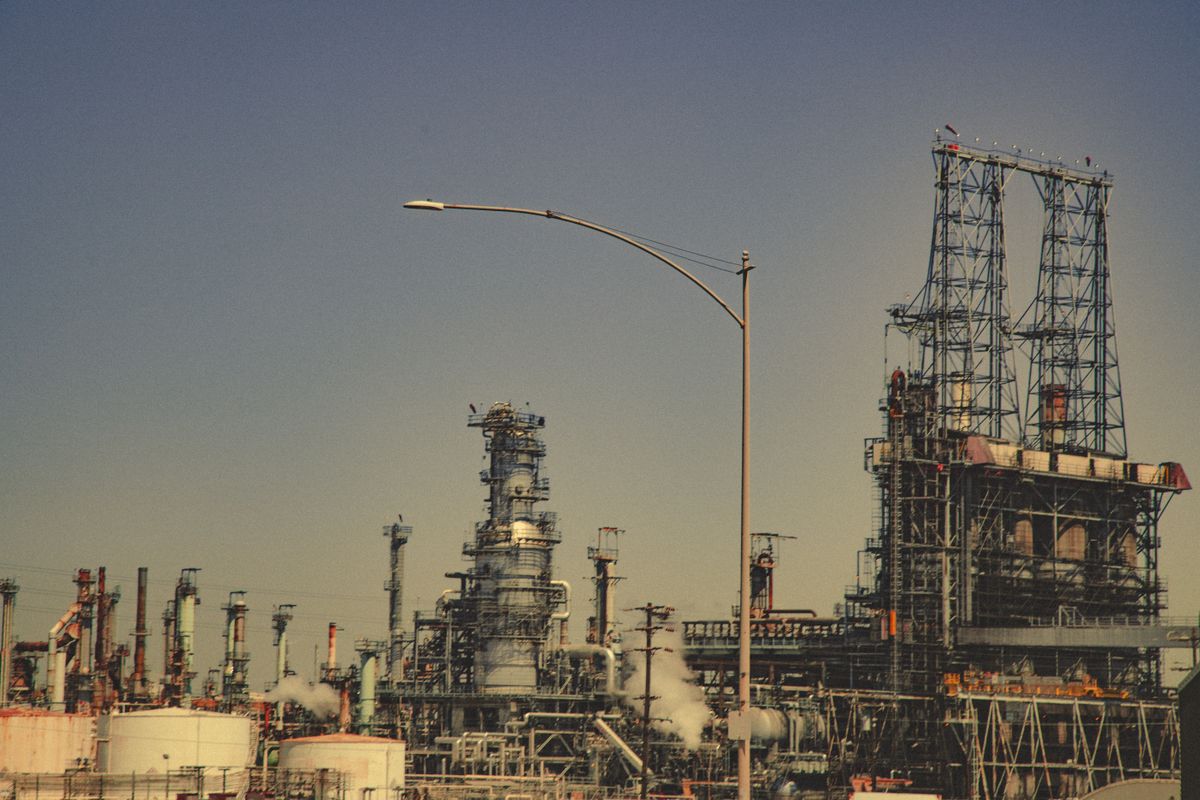 Manufacturing infrastructure
Scalable infrastructure for your growth
Our facility is configured to handle projects ranging from early-stage discovery to full commercial supply, with redundancy built in for continuity & reliability.
Systems aligned with global standards
Our quality management systems are designed & operated in alignment with internationally recognized standards, ensuring that every batch we produce meets the stringent requirements of regulatory filings worldwide.
ISO 9001 Certified
Quality management system certified to ISO 9001 for consistent, documented operations.
WHO-GMP Aligned
Manufacturing practices aligned with WHO Good Manufacturing Practice guidelines for pharmaceutical products.
REACH Compliance
Awareness & adherence to REACH chemical safety registration & documentation requirements.
ICH Guidelines
Documentation, stability protocols, & analytical validation aligned with International Council for Harmonisation standards.
cGMP Practices
Current Good Manufacturing Practice protocols built into our synthesis, process control, & quality systems.
Audit Readiness
Documentation systems, traceability, & change management designed to withstand regulatory inspection.
Methanol License
Licensed by the Drug Control Department for the procurement, storage, & use of methanol in manufacturing.
Ethanol License
Licensed by the Excise Department for the procurement, storage, & use of ethanol in manufacturing.
Every batch, fully documented
Comprehensive batch records, certificates of analysis (CoAs), technical data packages (TDPs), & process parameters are generated & archived for every production run. We maintain complete traceability of raw materials, reagents, & process steps, creating an audit trail that regulators & inspectors expect to see.
Responsible chemistry, from lab to planet
Our commitment to safety & environmental stewardship is as rigorous as our commitment to chemistry. We invest in waste solvent recovery systems, energy-efficient equipment, continuous safety training, & green chemistry alternatives, ensuring that the molecules we make don't compromise the future of those who make them.
- ✓ Waste solvent recovery & recycling programs
- ✓ Energy-efficient equipment & process optimization
- ✓ Comprehensive occupational health & safety protocols